Customization and Innovation Capabilities
Design Flexibility and Rapid Prototyping
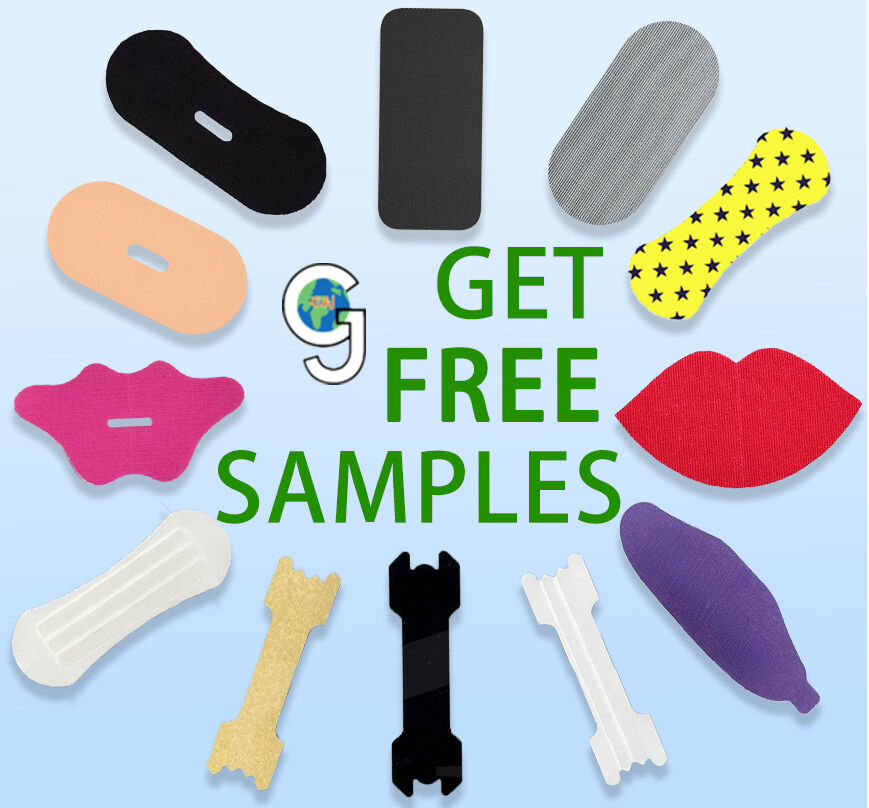
Leading manufacturers offer extensive customization options that allow clients to specify unique product characteristics including size variations, adhesive strength levels, and aesthetic elements such as color and printing. Computer-aided design capabilities enable rapid visualization of custom nasal strips configurations and facilitate customer approval processes before tooling commitments. Rapid prototyping services utilize 3D printing and small-batch production methods to validate designs and conduct preliminary testing.
Material experimentation programs explore novel substrate compositions and adhesive formulations that address specific performance requirements or target demographic preferences. These innovation initiatives often result in proprietary material combinations that provide competitive advantages for custom applications. Collaborative development programs engage customers in co-creation processes that leverage manufacturing expertise with market insights.
Scalable Production Planning
Effective manufacturing operations demonstrate flexibility in production scheduling and volume management to accommodate varying customer demand patterns. Modular production line designs enable rapid changeovers between different custom nasal strips configurations while minimizing setup times and material waste. Inventory management systems balance raw material availability with production capacity to ensure consistent delivery performance.
Capacity planning tools utilize historical demand data and market forecasts to optimize equipment utilization and workforce allocation. Strategic partnerships with material suppliers ensure reliable access to specialized components while maintaining cost competitiveness. Manufacturing execution systems provide real-time visibility into production status and enable proactive management of potential delays or quality issues.
Supply Chain Integration and Logistics
Supplier Qualification and Management
The manufacture of custom nasal strips requires sophisticated supplier networks that provide specialized materials and components meeting medical device standards. Supplier qualification programs evaluate technical capabilities, quality systems, and regulatory compliance status to ensure consistent material quality and supply continuity. Strategic sourcing initiatives balance cost optimization with performance requirements and supply chain risk mitigation.
Vendor audit programs include on-site assessments of manufacturing facilities, quality control procedures, and documentation systems. Long-term partnership agreements with key suppliers enable collaborative development of improved materials and cost reduction initiatives. Contingency planning identifies alternative suppliers and maintains qualified backup sources for critical materials to prevent production disruptions.
Global Distribution Networks
Manufacturing facilities serving international markets implement sophisticated logistics systems that manage complex shipping requirements and regulatory documentation across multiple jurisdictions. Temperature-controlled storage and transportation capabilities preserve product integrity during extended distribution cycles. Customs clearance expertise ensures efficient border crossings and minimizes delays that could impact customer delivery schedules.
Regional distribution centers enable local inventory management and rapid response to customer orders while reducing transportation costs and delivery times. Track and trace systems provide complete visibility into shipment status and enable proactive communication with customers regarding delivery schedules. Returns processing capabilities handle product recalls or quality issues efficiently while maintaining regulatory compliance and customer satisfaction.
Technology Integration and Industry 4.0
Smart Manufacturing Systems
Advanced manufacturing facilities incorporate Industry 4.0 technologies that enhance production efficiency and quality control capabilities for custom nasal strips production. Internet of Things sensors monitor equipment performance, environmental conditions, and process parameters in real-time to enable predictive maintenance and optimize production settings. Machine learning algorithms analyze historical production data to identify optimization opportunities and predict quality issues before they occur.
Digital twin technologies create virtual representations of manufacturing processes that enable simulation and optimization without disrupting actual production operations. These systems facilitate rapid evaluation of process changes and support continuous improvement initiatives. Cloud-based data analytics platforms aggregate information from multiple production lines and facilities to provide comprehensive performance insights and benchmarking capabilities.
Cybersecurity and Data Protection
Modern manufacturing operations implement robust cybersecurity measures to protect proprietary formulations, customer information, and operational data from unauthorized access or theft. Network segmentation isolates critical production systems from external connections while enabling necessary data sharing for supply chain coordination and customer communication. Regular security assessments identify vulnerabilities and ensure compliance with industry standards and customer requirements.
Data backup and recovery systems ensure business continuity in the event of system failures or cyber incidents. Employee training programs maintain awareness of cybersecurity best practices and promote responsible handling of sensitive information. Incident response procedures enable rapid containment and remediation of potential security breaches while minimizing operational disruptions and customer impact.
FAQ
What manufacturing capabilities are essential for producing high-quality custom nasal strips
Essential manufacturing capabilities include precision die-cutting equipment, controlled environment adhesive coating systems, automated assembly lines with vision inspection, and comprehensive quality control laboratories. Facilities must maintain clean room environments, implement robust supply chain management, and demonstrate regulatory compliance across multiple international markets. Advanced material processing capabilities and rapid prototyping services enable customization while maintaining production efficiency.
How do manufacturers ensure consistent quality across different custom nasal strips specifications
Quality consistency relies on standardized process controls, automated monitoring systems, and comprehensive testing protocols that evaluate both raw materials and finished products. Statistical process control methods track key performance indicators and trigger corrective actions when parameters drift outside acceptable ranges. Supplier qualification programs ensure material consistency while change control procedures prevent unauthorized modifications that could impact product quality.
What role does regulatory compliance play in custom nasal strips manufacturing
Regulatory compliance forms the foundation of legitimate custom nasal strips manufacturing, requiring adherence to medical device standards including ISO 13485 quality management systems and biocompatibility testing protocols. Manufacturers must maintain detailed documentation supporting product safety and efficacy claims while enabling customer regulatory submissions. Compliance capabilities directly impact market access and determine the ability to serve customers in regulated healthcare markets.
How do manufacturing facilities accommodate varying volume requirements for custom nasal strips orders
Flexible manufacturing systems utilize modular production line designs that enable rapid changeovers between different product configurations while optimizing equipment utilization. Scalable capacity planning incorporates demand forecasting and inventory management to balance production efficiency with customer delivery requirements. Strategic partnerships and contract manufacturing relationships provide additional capacity options for large orders while maintaining cost competitiveness across varying volume levels.